Digital Multimeters for PCB Troubleshooting

A 10-ohm reading can mean a healthy current-sense resistor, a shorted IC rail, or simply the resistance of test leads and probe contact. That is why digital multimeters remain the first instrument reached for at the bench, but not always the last instrument needed. For PCB troubleshooting, production inspection, and field service, the value of a meter depends less on its number of functions than on how reliably it resolves the measurement in front of you.

What Digital Multimeters Do Well

Digital multimeters measure the electrical quantities that establish whether a circuit has the conditions needed to operate: DC and AC voltage, resistance, current, continuity, and usually diode forward voltage. Many professional models also include capacitance, frequency, duty cycle, temperature, and non-contact voltage detection.

For electronics work, voltage measurement is often the starting point. A technician can verify a 3.3 V regulator output, trace a missing bias supply, compare a reference rail against a schematic, or confirm that a battery-backed circuit is receiving power. Resistance and continuity measurements then help locate open traces, damaged fuses, poor connector contacts, and unintended shorts.

A diode-test function is especially useful on populated boards. It applies a controlled test current and displays the forward voltage of a diode junction. Comparing readings across matched transistor junctions, ESD protection devices, MOSFET body diodes, or parallel channels can reveal an abnormal device quickly. The interpretation still requires circuit awareness, because parallel components may alter the reading.

Specifications That Determine Useful Measurements

A long feature list does not compensate for weak basic specifications. When selecting a meter for professional work, start with accuracy, resolution, input behavior, protection, and measurement speed.

Accuracy and resolution are different

Basic DC voltage accuracy states how close a reading is expected to be to the actual value under defined conditions. A specification of ±0.1% is materially different from ±0.5% when verifying precision references, sensor outputs, or low-voltage power rails. The full specification also includes counts, such as ±(0.1% + 2 counts), which becomes more significant near the bottom of a range.

Resolution is the smallest display change the meter can show. A meter may display 0.001 V, but that does not mean the reading is accurate to 1 mV. Resolution is valuable when observing small changes, such as voltage drop across a shunt or drift on an analog control line. Accuracy determines how much confidence to place in the displayed value.

For routine board repair, a well-specified 4,000- or 6,000-count meter may be sufficient. For calibration checks, low-level analog work, or detailed power-rail diagnosis, higher counts and better DC accuracy can reduce ambiguity. More digits are useful only when noise, probe contact, and the circuit itself support the measurement.

Input impedance and burden voltage affect the circuit

A voltmeter is not completely invisible to the circuit under test. Input impedance determines the load it places on a voltage source. High input impedance is generally preferred for electronics measurements because it minimizes loading, particularly on high-resistance dividers, sensor circuits, and reference nodes.

Current measurement has a different trade-off. The meter inserts an internal shunt resistance into the circuit, creating burden voltage. On a low-voltage device, that drop can change circuit operation or prevent startup. Before measuring current in series, consider whether a current-sense resistor, a clamp accessory, or a measured voltage drop provides a less intrusive method.

Protection is part of the specification

Input protection is not a convenience feature. It determines whether a meter can safely tolerate transients and incorrect connections in the environment where it will be used. Category ratings, fused current ranges, high-energy fuses, protective input design, and clearly separated current terminals matter most when servicing mains-powered equipment, industrial controls, or high-energy battery systems.

A higher category rating does not make every measurement safe. It must match the instrument’s rating, the correct input jack, the selected range, the probe rating, and the actual installation environment. On low-voltage PCB work, protection still matters because an accidental current-range connection across a powered rail can damage the board, the meter fuse, or both.

Functions That Matter at the PCB Bench

Continuity response time is easy to overlook until tracing connectors and vias across a dense assembly. A fast, decisive audible response keeps the operator focused on the board rather than the display. Slow continuity functions can make intermittent connections and short trace runs harder to assess.

Auto-ranging is convenient, but manual range selection can be better when readings fluctuate or when comparing repetitive measurements. A fixed range avoids range-hunting delays and makes small changes easier to see. Relative mode is also valuable for subtracting probe resistance, nulling a fixture, or comparing one channel against a known-good channel.

True RMS AC measurement is worthwhile when checking non-sinusoidal waveforms from switching supplies, motor drives, dimmers, or variable-frequency systems. A basic average-responding AC meter can produce misleading results on distorted waveforms. Even a true RMS meter has bandwidth limits, so its AC specification must cover the waveform frequency being measured.

Data hold, min/max capture, and logging can turn a handheld meter into a more useful diagnostic tool. Min/max capture helps identify supply dips during startup or intermittent voltage loss. Bluetooth-enabled instruments can transfer readings to a mobile device or PC, reducing transcription errors and making it easier to document test results during production or service work.

A Practical Measurement Sequence for Board Faults

Before applying power, inspect the board and use resistance or continuity mode to check for obvious shorts between supply rails and ground. Interpret low resistance carefully. Modern processors, large capacitor banks, and parallel ICs can legitimately present low readings, especially while capacitors charge from the meter’s test source.

With power applied, verify input power first, then work from the supply chain toward the load. Check fuse voltage drop, regulator input and output, enable pins, reference voltages, and local decoupling rails. Measure at the component pins when possible, not only at a distant test point. A trace, connector, ferrite bead, or damaged via can create a fault between the two locations.

For comparative troubleshooting, measure the same nodes on a known-good board and a suspect board. This method is often faster than relying on nominal values alone. Diode-mode comparisons are particularly effective for finding shorted semiconductor junctions or abnormal rail-to-ground behavior when the equipment is unpowered.

Use appropriately sized probes and sharp tips for fine-pitch boards. Standard probes can bridge adjacent pins or slip from small test pads. Dedicated probing accessories and tweezer-style instruments improve component access where conventional leads are physically awkward. Siborg Systems instruments are designed around this component-level workflow, particularly for SMD measurement and direct PCB access.

Where a Multimeter Reaches Its Limit

Digital multimeters provide a numerical value, but they do not show waveform shape, timing, ripple, or transient behavior. A 5 V rail can measure correctly on a meter while carrying excessive switching noise or collapsing for microseconds during a load transition. An oscilloscope is the proper next tool when waveform integrity is in question.

Likewise, resistance and capacitance modes do not replace dedicated LCR or ESR measurement for component characterization. In-circuit capacitance readings can be affected by parallel paths, semiconductor junctions, and charge stored on the board. ESR, inductance, dissipation factor, and test frequency become relevant when diagnosing switching power supplies, filter networks, and small passive components.

The strongest workflow uses each instrument for what it measures best. Use the multimeter to establish DC conditions and isolate obvious faults. Use an LCR meter, ESR meter, or test tweezers to identify passive components and verify their values. Use a scope or analog signature analysis when the fault is dynamic or interaction-dependent.

Selecting a Meter for the Actual Job

Choose digital multimeters by the circuits you service, not by the largest advertised function count. A field technician working around distribution panels needs category-rated protection and dependable AC performance. A PCB repair specialist benefits from high DC accuracy, fast continuity, stable low-resistance measurement, fine probes, and a display that remains readable while probing. Manufacturing and quality teams may prioritize repeatability, calibration documentation, data capture, and controlled test procedures.

NIST-traceable calibration documentation is particularly relevant when readings support production acceptance, maintenance records, or quality systems. Calibration does not eliminate the need for proper technique, but it establishes a documented basis for measurement confidence.

A meter earns its place on the bench when it shortens the path from symptom to evidence. Select one that matches the voltages, tolerances, safety environment, and board density you encounter, then pair it with probes and specialized instruments that let you measure the component rather than merely reach the circuit.
Benchtop Versus Handheld LCR Meters: Which Fits?

A failed 0402 capacitor on a densely populated board does not become easier to diagnose because a laboratory LCR meter has excellent published specifications. The immediate question is whether its test fixture can reach the part without removing it. That is the practical distinction behind benchtop versus handheld measurement: the best instrument is the one that produces a meaningful result at the point where the component must be tested.

For engineering validation, incoming inspection, production quality control, and PCB repair, both instrument types have valid roles. The trade-off is not simply accuracy against portability. It involves test frequency, fixture compensation, contact geometry, measurement speed, bias requirements, data handling, and whether the component is loose or installed in a circuit.

Benchtop Versus Handheld: Start With the Measurement Task

A benchtop LCR meter is generally designed for controlled measurement. It is at home on an ESD-safe bench with dedicated test fixtures, guarded connections, programmed test conditions, and a repeatable operator process. For loose components, particularly when values must be compared against a specification or recorded for quality documentation, that environment is valuable.

A handheld LCR meter is designed to put the measurement point in the technician’s hand. Its advantage is direct access to components on a PCB, in an assembly, or in the field. With integrated probes or tweezer-style contacts, the operator can identify resistance, capacitance, inductance, ESR, impedance, and related parameters without arranging conventional test leads around small pads.

Neither format automatically produces a better measurement. A high-grade handheld instrument can provide basic accuracy appropriate for professional component work, while a benchtop instrument can produce misleading data if the fixture is poorly compensated or the component is tested under irrelevant conditions. The decision should begin with the component, test condition, and workflow rather than the physical size of the instrument.

Where Benchtop Instruments Have a Clear Advantage

Benchtop meters are the stronger choice when measurement repeatability must be controlled across operators, batches, or extended test sequences. A fixed fixture reduces variation in contact force, lead placement, and parasitic effects. This is particularly useful for low-value inductors, high-Q components, precision capacitors, and measurements where small changes in impedance or dissipation factor matter.

They also support workflows that need more elaborate test setups. Depending on the model, a benchtop instrument may offer a broad range of frequencies, AC test levels, DC bias functions, binning, limit testing, remote control, and automated data collection. These capabilities matter in component characterization, production screening, and design verification.

The physical test setup is part of the advantage. Kelvin fixtures, guarded terminals, shielded cables, and open/short/load compensation help control errors introduced by leads and contacts. When a part is loose and the measurement must be repeated hundreds or thousands of times, the benchtop approach is efficient and defensible.

There is also a practical ergonomic benefit in long measurement sessions. Operators can place reels, trays, or individual parts in a dedicated fixture rather than holding probes manually. That consistency can outweigh the time required to move a component from the assembly area to the bench.

Limits of the Benchtop Workflow

The limitation is access. A benchtop meter cannot directly solve the problem of a suspect component located between fine-pitch ICs, under a shield edge, or on a board that cannot be removed from service. Standard test leads add length and inductance, and clips can be too large for modern surface-mount work.

In-circuit measurements introduce another limitation: the reading represents the surrounding circuit as well as the target component. A parallel resistor can lower the apparent resistance. A capacitor tied to a power rail may be measured alongside several other capacitors. No instrument format eliminates circuit interaction, but direct probing makes it faster to compare locations, isolate a suspect area, and determine whether lifting one terminal is necessary.

Where Handheld Meters Improve PCB Diagnostics

Handheld instruments earn their place when diagnosis depends on speed and component access. A technician investigating a shorted rail, incorrect capacitor placement, damaged inductor, or questionable resistor does not always need a fully automated fixture. They need stable contact on a small component and enough relevant information to make the next repair decision.

Tweezer-style LCR meters are particularly effective for loose SMD parts and accessible components on populated boards. The two probe tips form the measurement contacts, allowing the user to grip an 0201, 0402, or larger component directly. This eliminates the time spent positioning clips and reduces the chance of probing adjacent pads.

Test frequency is central to this application. A capacitor’s apparent value and ESR can change significantly with frequency, while inductors and ferrites may show behavior that a low-frequency measurement does not reveal. A handheld meter with test frequencies up to 100 kHz or 250 kHz can provide more useful diagnostic information for switched-mode power supplies, high-frequency decoupling networks, and RF-related assemblies than a basic low-frequency handheld tester.

Basic accuracy also matters, but it should be evaluated in context. A specified 0.1% or 0.2% basic accuracy is meaningful only when the selected range, test frequency, component value, calibration status, and connection method support the measurement. For repair work, repeatable comparison is often as valuable as absolute precision. Measuring a known-good channel against a failed channel can identify an abnormal component even when in-circuit conditions prevent a final standalone value.

Features That Extend a Handheld Instrument Beyond LCR

The strongest handheld tools combine multiple diagnostic functions instead of forcing the user to change instruments for every step. ESR measurement helps identify degraded electrolytic capacitors. Diode and LED testing support quick checks of semiconductors and lighting assemblies. Continuity and resistance functions assist with tracing opens, shorts, and damaged connections.

Advanced models can add oscilloscope capability or Analog Signature Analysis. These functions are not replacements for a dedicated bench oscilloscope or curve tracer in every application. They are compact diagnostic tools that help technicians compare waveform activity or component signatures without leaving the board-level troubleshooting process.

Bluetooth connectivity can also be practical rather than decorative. Capturing readings on a mobile device or PC supports documentation, training, quality records, and remote technical review. Faster Bluetooth communication is especially useful when measurements are collected continuously or when an operator needs to observe changing values without reading a small display at an awkward angle.

Siborg Systems’ Smart Tweezers and LCR-Reader instruments reflect this workflow: professional measurement capability is packaged around direct component contact, high test-frequency options, and accessories intended for PCB work.

Accuracy Is Not the Same as Confidence

A common purchasing mistake is to compare only the highest accuracy number on a datasheet. The more useful question is: what uncertainty enters the result in the actual application?

For a benchtop meter, uncertainty can come from fixture compensation, cable condition, test signal settings, component orientation, temperature, and operator procedure. For a handheld meter, probe contact quality, surface contamination, component size, battery condition, and in-circuit loading may have greater influence. A clean measurement process reduces these variables more effectively than selecting a meter based on one headline specification.

Calibration is part of that process. For work requiring traceable results, a NIST Traceable Calibration Certificate provides documented support for the instrument’s performance. It does not correct poor probing technique or make an in-circuit value equivalent to an isolated component measurement. It does establish a verified reference point for quality systems, service organizations, and professional laboratories.

Choose by Workflow, Not by Instrument Category

A benchtop LCR meter is usually the better investment when the work centers on loose components, incoming inspection, formal characterization, production tests, or repeatable fixture-based measurements. It is the right tool when test conditions must be tightly defined and documented.

A handheld instrument is usually the better first choice when the work centers on PCB repair, field service, prototype debugging, component identification, and fast inspection of surface-mount parts. It is particularly effective when removing a component just to obtain a preliminary measurement would slow diagnosis or risk board damage.

Many professional environments need both. The handheld unit identifies the suspect component at the board. The benchtop meter verifies the removed part under controlled conditions. That division of labor is often more efficient than asking either instrument to do every job.

Before selecting a meter, test it against the actual components and assemblies you handle most often. The instrument that reaches the part, applies the relevant frequency, delivers repeatable readings, and fits your documentation requirements will provide the measurement confidence that matters on the bench and in the field.

Multimeter Versus Component Analyzer Compared

A failed 0402 capacitor does not announce itself with a convenient pair of test pads. On a densely populated board, the technician must reach a part, identify it, and decide whether its measured behavior is credible without losing time to lead placement or removing components prematurely. That is where the multimeter versus component analyzer decision becomes practical rather than theoretical.

A digital multimeter remains the first instrument many technicians reach for, and for good reason. It is the correct tool for verifying supply rails, continuity, voltage drops, current, diode junctions, and basic resistance. A component analyzer, particularly an LCR or ESR instrument with tweezer probes, addresses a different measurement problem: determining the value and electrical characteristics of a component quickly, often directly on the PCB.

Neither tool replaces the other. The correct choice depends on whether the fault is in the circuit’s operating conditions or in an individual component.

Multimeter versus component analyzer: the essential difference

A multimeter measures broad electrical quantities. In board-level troubleshooting, it answers questions such as: Is the 3.3 V rail present? Is this trace open? Is the fuse intact? Does this diode conduct in the expected direction? Is there a short between power and ground?

A component analyzer is designed to characterize parts. Depending on the instrument and mode, it can identify resistance, capacitance, inductance, ESR, impedance, dissipation factor, and sometimes component type. Advanced handheld instruments can also provide test frequencies appropriate for evaluating small capacitors and inductors beyond a simple low-frequency measurement.

This distinction matters because a component can pass a basic multimeter check and still be unsuitable in its circuit. A ceramic capacitor may not be shorted, but its capacitance may be far below value. An inductor may show continuity while its inductance is incorrect. A low-value resistor can be difficult to measure accurately with standard leads because probe and contact resistance become part of the result.

Where a digital multimeter remains the right first tool

For energized-board diagnostics, the multimeter is usually indispensable. It is designed to measure DC and AC voltage safely, and it can reveal whether a circuit section is receiving power before a technician begins evaluating individual parts. A component analyzer is not a substitute for verifying a regulator output, measuring a bias voltage, or checking current draw in series with a supply.

Continuity mode is also highly effective for locating broken traces, damaged connectors, open fuses, and solder-joint failures. Diode mode provides a fast comparison method for semiconductor junctions and parallel devices. These are circuit-level tests, not component-characterization tests.

A multimeter is also often the better choice when measurement category, input protection, and a wide voltage range are required. Professional troubleshooting starts with safety and with an understanding of the circuit state. Before touching an unpowered board with an LCR or ESR instrument, discharge capacitors and confirm that no external supply is present.

The limitation is resolution at the component level. Standard probes can slip on fine-pitch pads, bridge adjacent SMD parts, and add variable contact resistance. The meter may display resistance, capacitance, or diode behavior, but its available test conditions may not match the conditions that expose the suspected failure.

What a component analyzer adds to PCB work

A component analyzer shortens the path from suspected part to usable measurement. With tweezer-style probes, an operator can contact both ends of an SMD resistor, capacitor, or inductor directly. The instrument can identify the component category and display the relevant value without changing leads or manually selecting a function in many cases.

That workflow is especially valuable during incoming inspection, rework verification, repair of consumer and industrial electronics, and production troubleshooting. Instead of removing a part simply to read its value, a technician can obtain an initial in-circuit result in seconds. The result may not always be the final answer, but it is often enough to prioritize the next diagnostic step.

Frequency is one of the major differentiators. Capacitance and inductance are not fixed, context-free numbers. Their measured behavior changes with test frequency, bias, parasitics, and construction. A meter limited to a basic capacitance function may confirm a gross failure but may not provide useful discrimination among small, high-frequency components. Instruments offering 100 kHz or 250 kHz test frequencies can provide more relevant characterization for many SMD capacitors and inductors used in modern electronics.

ESR measurement is another example. A capacitor can retain a nominal capacitance reading while excessive equivalent series resistance impairs filtering or switching-supply performance. Measuring ESR at an appropriate frequency gives repair personnel a more meaningful indication of capacitor condition than capacitance alone.

In-circuit measurements require judgment

The phrase in-circuit measurement needs a qualification. A component analyzer measures the electrical network presented at its probes, not a magically isolated part. Parallel resistors, bypass capacitors, semiconductor paths, and nearby circuitry can alter the displayed value.

For example, a 10 kOhm resistor may read lower because another resistance path exists in parallel. A capacitor may read higher than expected when neighboring capacitors share the same rail. An inductor measurement can be affected by its surrounding switching converter circuitry. A correct reading in circuit is useful evidence, but an unexpected reading is not automatically proof that the contacted component has failed.

Experienced technicians use comparison. Measure an identical channel, a known-good board, or the same component position in a repeated circuit section. If the suspected capacitor reads 2.1 uF while equivalent locations read near 10 uF, the result is actionable even if the exact in-circuit value differs from the marking or schematic value.

When accuracy is critical, isolate one terminal or remove the part. This is not a weakness of the instrument. It is a property of network measurement. The best workflow uses rapid in-circuit screening first, then isolates only the parts that require confirmation.

Probe geometry can matter as much as accuracy

A published basic accuracy specification is necessary, but it is only part of real-world measurement quality. On 0201, 0402, and fine-pitch components, the ability to make stable, repeatable contact determines whether that specification can be achieved at the board.

Traditional test leads are flexible and universal, but they require two hands or a fixture and can obscure the target. Tweezer probes place both contacts under controlled spacing, improving access to small parts and reducing the risk of probing adjacent pads. This can materially improve throughput when hundreds of component checks are required.

For low-resistance work, contact resistance and lead compensation are equally significant. A reading of a few tenths of an ohm can be dominated by the test setup unless the instrument provides appropriate compensation and the operator maintains clean, firm contact. For precision work, verify calibration status and use an instrument supplied with a NIST-traceable calibration certificate when documentation is required by a quality system.

Siborg Systems instruments such as Smart Tweezers and LCR-Reader models are built around this direct-contact workflow, combining automatic component recognition with handheld LCR measurement for loose and board-mounted parts. Model selection should still follow the work: higher test frequency, Bluetooth data transfer, oscilloscope capability, or Analog Signature Analysis are valuable when they support the actual diagnostic process rather than merely adding functions.

Choosing the instrument for the failure mode

Use a multimeter when the immediate question concerns voltage, current, continuity, a power path, or a semiconductor junction. It establishes whether the circuit is powered correctly and whether obvious opens or shorts exist. It is the general-purpose foundation of every electronics bench and field kit.

Use a component analyzer when the question concerns the value or health of a resistor, capacitor, inductor, or other discrete component, especially a small SMD device. It is the faster choice when lead placement, measurement frequency, ESR, component identification, and repeatability on populated PCBs determine diagnostic speed.

For difficult faults, use both in sequence. Check the rail and circuit condition with the multimeter. Then use the analyzer to compare suspect components against expected values or a known-good reference. If the readings conflict with the schematic or with equivalent channels, isolate the part and measure it again.

The useful instrument is the one that reduces uncertainty at the next decision point. Keep the multimeter ready for circuit-level facts, and keep a component analyzer within reach when the diagnosis narrows to the parts themselves.

How to Measure Diode Forward Voltage Accurately

A diode that reads 0.62 V in diode mode may be perfectly healthy, while a 0.28 V reading may also be correct. The difference is not a meter error by default. To understand how to measure diode forward voltage, you need to account for diode type, test current, junction temperature, and whether the device is still connected to a circuit.

For troubleshooting, a digital multimeter’s diode-test function is usually the fastest first check. For characterization, LED verification, or comparison against a production specification, the test method must define current and temperature. Forward voltage is not a fixed property stamped onto the component. It is the voltage drop across a forward-biased PN junction at a particular current.

What diode forward voltage actually represents

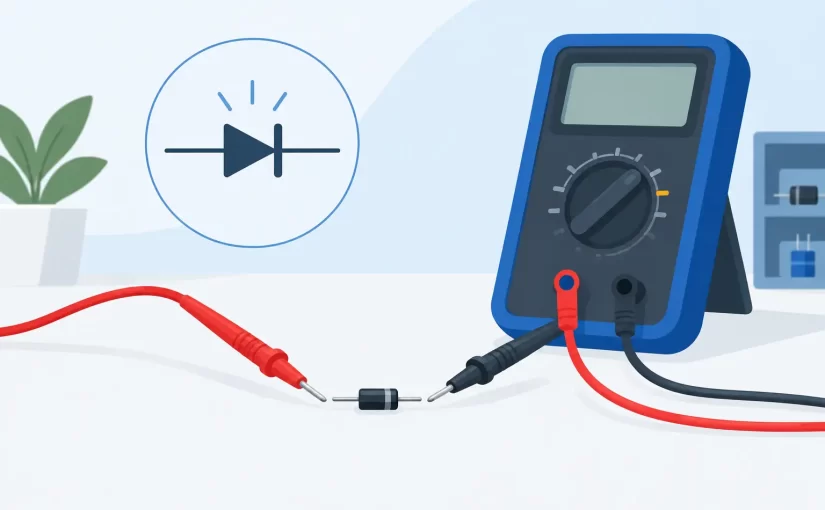
A diode conducts when its anode is at a higher potential than its cathode. In that forward-biased condition, the junction develops a voltage drop called forward voltage, commonly written as Vf. A meter in diode mode applies a small, controlled test current and displays the resulting voltage.

That detail matters. A silicon switching diode may display approximately 0.55 to 0.80 V at a multimeter’s low test current, yet operate at a different forward voltage when carrying its rated circuit current. A rectifier diode, Schottky diode, germanium diode, and LED all have different expected ranges.

Temperature also changes the result. For a conventional silicon PN junction, forward voltage generally decreases as junction temperature rises. Comparing readings is most useful when the same meter, test current, and approximate temperature are used for each component.

How to measure diode forward voltage with a multimeter

Use a DMM with a dedicated diode-test setting rather than a resistance range. Resistance mode can indicate gross shorts or opens, but it does not provide a controlled, interpretable forward-voltage result.

Prepare the circuit and instrument

Turn off circuit power before connecting the meter. Disconnect batteries, remove external supplies, and discharge capacitors where stored energy is possible. A charged electrolytic capacitor can produce misleading readings or damage a meter input.

Set the multimeter to diode mode, normally marked with a diode symbol. Check the meter manual if the symbol shares a switch position with continuity. Some instruments require a function-button press to select diode test.

For a loose component, identify the terminals before probing. The cathode of many axial diodes is marked by a band. On SMD diodes, cathode marking may be a line, a dot, a beveled edge, or a package-specific code. Verify the package documentation when the marking is unclear, especially with small SOT and DFN devices.

Apply the probes in the forward direction

Place the red probe on the anode and the black probe on the cathode. Most modern DMMs source current from the red probe in diode mode, but confirm this behavior on an unfamiliar instrument using a known diode.

The display should settle on a voltage value. Record the value in volts. For example, a display of 0.647 means 647 mV of forward voltage at that meter’s diode-test current.

Reverse the probes next. A good diode should normally display OL, an overload indication, or a reading far outside the forward result. This reverse-direction check is essential because a forward reading alone cannot distinguish every failure mode.

Interpret the basic results

A useful first-pass interpretation is straightforward:

  • A normal forward reading and OL in reverse usually indicate a functioning diode.
  • A reading near 0 V in both directions suggests a shorted junction.
  • OL in both directions suggests an open diode, incorrect probe contact, or a meter whose diode-test voltage cannot overcome the device’s threshold.
  • Similar nonzero readings in both directions often indicate a parallel circuit path rather than a failed diode.

These are diagnostic patterns, not final component specifications. Measure against the device datasheet when acceptance limits matter.

Expected readings by diode type

Standard silicon signal and rectifier diodes commonly read about 0.55 to 0.80 V in a handheld meter’s diode mode. Higher-current rectifiers can differ from small-signal parts because of die construction and the meter’s test current.

Schottky diodes often read lower, commonly about 0.15 to 0.45 V. Their lower forward drop is a design advantage in power conversion, but it also means that a low reading is not automatically evidence of a short. Compare the result with the specified part type.

Germanium diodes may read roughly 0.20 to 0.35 V. They also have higher leakage than silicon devices, so reverse readings can require more careful interpretation.

LEDs require additional context. A red LED may measure around 1.6 to 2.1 V, while blue, white, and many ultraviolet LEDs may require 2.8 to 3.6 V or more. Many handheld meters cannot provide enough open-circuit test voltage to forward-bias higher-voltage LEDs. An OL display in diode mode can therefore mean either an open LED or an instrument limitation.

When testing LEDs, use an LED tester or a controlled current source if the meter cannot drive the device. The target is a defined current and an observed Vf, not simply obtaining any illuminated condition.

Why in-circuit diode measurements can mislead

Testing a diode on a populated PCB is efficient, but the circuit around it can create alternate paths. Resistors, IC input protection structures, transformer windings, capacitors, and other semiconductor junctions may all affect the displayed value.

A diode across a motor coil or relay coil, for example, may be influenced by the coil resistance and associated suppression circuitry. A diode inside a power supply may have parallel paths through MOSFET body diodes, controller ICs, or transformer windings. In these cases, the meter is measuring the network, not just the intended junction.

Start with an in-circuit check when access is limited and use it as a comparison tool. Compare identical channels, phases, or board sections when possible. If the result is ambiguous, lift one diode lead or remove the component for a definitive measurement. Lifting one terminal is normally sufficient to eliminate most parallel paths while reducing rework compared with full removal.

For small surface-mount parts, probe placement is often the limiting factor. Fine test tips or tweezer-style contacts reduce the chance of touching adjacent pads and provide more repeatable contact pressure. Siborg Systems instruments are designed for direct access to small PCB components where conventional probes can be slow and imprecise.

Match the measurement method to the job

A DMM diode test is appropriate for rapid fault isolation: open versus short, polarity confirmation, and rough comparison between similar devices. It is not a replacement for a datasheet-defined forward-voltage test.

For a controlled Vf measurement, use a regulated current source set to the relevant operating or inspection current. Connect the diode in series with the source, allow the reading to stabilize, and measure voltage directly across the diode terminals with a high-input-impedance voltmeter. Keep the test duration short for power devices and high-current LEDs because self-heating shifts Vf.

The datasheet condition should drive the setup. If a diode specifies Vf maximum at 1 A and 25 C, a measurement at 1 mA in a DMM tells you little about compliance at 1 A. Conversely, forcing a small signal diode to a high current simply to imitate a power-device test can destroy it.

For production or incoming inspection, document the test current, ambient temperature, fixture contact method, polarity, settling time, and pass limits. Repeatability depends as much on these controls as on meter resolution. A calibrated instrument supports traceability, but calibration cannot correct an undefined test condition.

Common measurement errors to avoid

The most frequent error is using continuity mode and assuming the beep confirms a good diode. Continuity thresholds vary by meter and may beep for a low-voltage Schottky diode, a partial short, or an unintended parallel path. Read the actual diode-mode voltage instead.

Another error is treating a typical forward voltage as an absolute pass/fail number. A 0.70 V silicon diode is not universally good, and a 0.30 V diode is not universally bad. Part family, current, temperature, and board context determine what is plausible.

Poor contact can also look like an open junction. Oxidized leads, conformal coating, damaged SMD pads, and probe slip add uncertainty. Clean the accessible contact point and hold probes steadily before calling a component defective.

A forward-voltage reading becomes valuable when it is tied to a known test condition and compared with the right reference: the datasheet, a verified-good board, or an identical component measured the same way. That discipline turns a quick meter check into evidence you can use for repair, quality control, and failure analysis.

How to Test LED Strips Without Guesswork

A backlight can appear completely dead when only one LED in a series string has opened. A strip can also test good on the bench yet fail in the product because its connector, current driver, or thermal path is the actual fault. Knowing how to test LED strips means separating the strip itself from the power and control circuitry, then applying enough voltage and current control to produce a meaningful result without overstressing the LEDs.

This procedure applies to common constant-current LED strips used in LCD TV backlights, signage, appliances, under-cabinet fixtures, and general lighting. Addressable RGB strips require a different approach because they contain integrated control ICs, but the same basic checks for supply voltage, continuity, and physical damage still apply.

Start with the strip type and its electrical rating

Before connecting a meter or power source, identify whether the strip is a low-voltage parallel design or a high-voltage series string. This determines what a normal reading looks like and what test equipment is appropriate.

A 12 V or 24 V flexible lighting strip normally has repeated segments. A 12 V single-color segment often contains three LEDs and one resistor, while a 24 V segment may use six LEDs or another series-parallel arrangement. These strips can usually be evaluated section by section with a multimeter diode function, provided the strip is disconnected from its controller.

LCD backlight strips are different. They commonly use many white LEDs wired in series, sometimes with several series strings in parallel. One white LED has a forward voltage near 2.7 V to 3.3 V at modest current. A 10-LED string may therefore require roughly 30 V, while a long TV strip assembly can require well over 100 V. Do not attempt to power an unknown backlight strip from an unregulated high-voltage source.

Read the markings on the PCB, label, or original power supply. Record the polarity, rated input voltage, strip part number, and connector pin count. If there are multiple channels, identify whether each pair of terminals feeds an independent string.

Inspect before applying power

Visual inspection is not a substitute for measurement, but it often determines where to measure first. Look closely at each LED package, solder joint, copper trace, connector, and resistor. A browned PCB, lifted pad, cracked lens, darkened phosphor, or blistered LED lens is strong evidence of a local thermal failure.

For flexible strips, bends near connectors and cut points deserve particular attention. Copper traces can crack beneath the solder mask, producing an intermittent open that looks normal until the strip is flexed. On rigid aluminum-core backlight strips, check for corrosion around lenses, damage from prying tools, and poor contact between the strip and its heat-spreading chassis.

If a failed LED has been replaced previously, inspect the repair for correct polarity and adequate solder wetting. An LED installed backward will block the entire series string. Excess solder can also bridge pads or interfere with lens placement.

Test individual LEDs with a multimeter

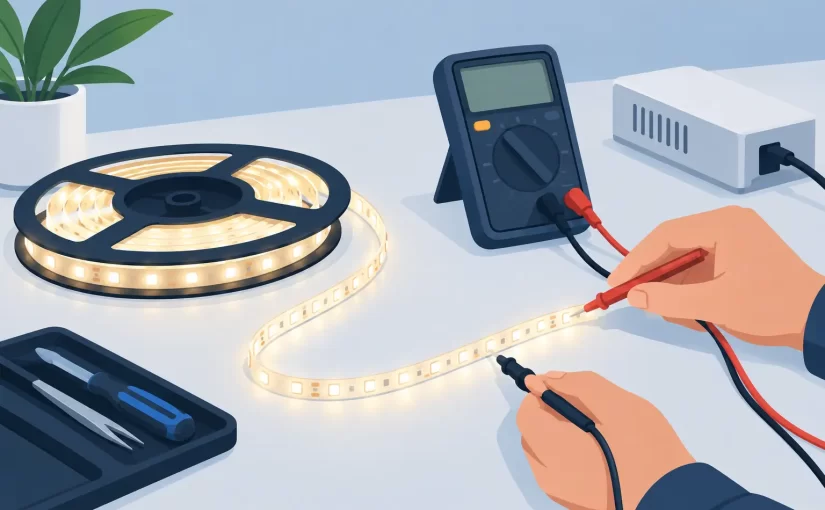
A digital multimeter diode mode is the fastest first test for accessible LEDs. Disconnect the strip from all power and control boards. Place the red probe on the LED anode and the black probe on the cathode. Many meters source enough current to make a healthy low-power LED glow faintly. A white backlight LED may show a forward-voltage reading, glow briefly, or show overload because the meter’s diode-test voltage is too low.

Reverse the probes. A healthy LED should not conduct significantly in reverse. Compare readings with neighboring LEDs of the same type rather than relying only on one absolute number.

A reading near 0 V in both directions suggests a shorted LED or a solder bridge. An overload indication in both directions can mean an open LED, incorrect probe placement, poor contact, or insufficient diode-test voltage. Check the probes against a known-good LED before condemning the device.

For SMD LEDs, conventional pointed probes can slide off tiny pads and create inconsistent results. Fine-pitch probes or tweezer-style test instruments improve repeatability by contacting both terminals directly. This is especially useful when confirming whether one component is open while it remains on a populated board. Keep in mind that parallel circuit paths can affect an in-circuit reading. When a result is ambiguous, isolate one LED terminal or test the strip out of circuit.

Use a dedicated LED tester for series strings

An LED strip tester is the practical tool for testing long backlight strings. These instruments typically provide automatically adjusted DC voltage with current limiting, allowing a technician to energize a series string without calculating and assembling a high-voltage bench setup. Connect the tester to the marked positive and negative strip terminals, beginning with the lowest available current setting.

A good string should illuminate uniformly. Watch for one LED that is dimmer, a section that does not light, or a string that requires an unusually high or low voltage compared with an identical channel. Record the operating voltage shown by the tester. Comparison is valuable: two nominally identical strips should have similar forward-voltage requirements at the same test current.

Do not use the tester result alone to judge LED health. A string may illuminate at the tester’s low current but fail under normal operating current because of thermal damage, weak bonds, or marginal solder joints. If the product fails after a brief warm-up, run the strip at a controlled current and observe it for several minutes while monitoring temperature.

Test low-voltage strips by segment and current draw

For 12 V and 24 V strips, apply the rated voltage from a current-limited bench supply. Start with a conservative current limit, then raise it only as needed for normal illumination. The expected current depends on strip density and LED type, so compare against a known-good sample, manufacturer specification, or another undamaged section of the same installation.

If the entire strip is dark and the supply immediately enters current limit, disconnect it and measure resistance across the input. Very low resistance may indicate a shorted protection diode, reversed-polarity damage, a bridged solder joint, or a failed controller rather than failed LEDs.

If only one segment is dark, measure voltage at that segment while the strip is powered. A normal supply voltage across the segment with no light points to an open LED, open resistor, or failed connection within that section. No voltage at the segment points upstream to a broken trace, connector, switch, or control channel.

For RGB and RGBW strips, test each color channel independently. The common anode or common cathode configuration matters. A controller output that is pulse-width modulated may not produce a stable reading on a basic meter, so use a scope or meter with suitable duty-cycle capability when the control signal is in question.

Separate strip failures from driver failures

A functional LED strip does not prove that the installed system is functional. The driver must deliver the correct voltage or, for backlights, the correct regulated current. Measure at the driver output only when you understand the circuit and have suitable probes, meter ratings, and safe access.

For a constant-current driver, output voltage is a consequence of the connected LED string. An open string can cause the driver to rise toward its maximum compliance voltage and then shut down or cycle. A shorted LED can reduce required output voltage and may trigger fault protection. Therefore, a fluctuating output is not automatically a bad driver.

Check the driver input first. Confirm its DC supply, enable signal, dimming input, and connector integrity. Then compare the suspect channel with a known-good channel where possible. In a multi-string backlight system, swapping equivalent strip connectors can help determine whether the fault follows the strip or remains with the driver output. Power down before moving connectors.

A controlled test sequence prevents wasted repairs

Use this order when diagnosing an unknown assembly:

  • Inspect the strip, connector, and heat-damaged areas.
  • Identify the rated voltage, polarity, and series-string configuration.
  • Check individual accessible LEDs using diode mode.
  • Energize the isolated strip with a current-limited LED tester or bench supply.
  • Compare forward voltage, brightness, and current with a known-good channel.
  • Verify the installed driver’s input, enable, and output behavior only after the strip test is complete.

This sequence avoids a common mistake: replacing LEDs because the system is dark when the actual fault is a loose connector or disabled driver.

Handle test voltage and heat as measurement variables

LEDs are current-driven devices. Applying a fixed voltage without an appropriate current limit can destroy a healthy LED quickly, particularly when testing a single die or a short section. The correct test current depends on package size, thermal mounting, and the purpose of the test. A few milliamps may be enough to confirm polarity and emission. Evaluating brightness uniformity or operational heating requires a higher, controlled current.

Temperature changes forward voltage and can expose marginal parts. If a backlight strip works when cold but shuts down after warming, inspect for an LED with abnormal thermal behavior, poor aluminum-substrate contact, or a driver entering over-temperature protection. A thermal camera is useful, but careful observation and voltage comparison can still isolate many faults.

Siborg Systems’ component-level instruments are particularly suited to confirming small SMD parts and connections around LED assemblies, where stable, direct contact can matter as much as the measurement range. Use component measurements to support the fault diagnosis, not to replace a powered functional test.

A clear test record makes the repair repeatable: note strip part number, test current, forward voltage, ambient condition, and any channel-to-channel differences. The next time the same assembly arrives on the bench, those values turn an uncertain visual inspection into a fast, defensible decision.

How to Use Kelvin Probes for Accurate PCB Tests

A 0.05 ohm contact error is insignificant on a 10 kilohm resistor. On a 0.10 ohm current-sense resistor, it can invalidate the measurement. That is the practical reason to learn how to use Kelvin probes: they separate the current path from the voltage-sensing path, removing much of the error caused by test leads, clips, and probe contact resistance.

Kelvin probing is not a substitute for sound measurement practice. It is a four-terminal technique that improves results when the device under test has low resistance, low impedance, or when lead and contact resistance are a meaningful part of the reading. Used correctly, it is valuable for current shunts, battery tabs, cable joints, relay contacts, PCB traces, low-value resistors, and capacitor ESR measurements.

How to Use Kelvin Probes: The Four-Wire Principle

A conventional two-wire measurement sends test current through a pair of leads and measures voltage through those same leads. The instrument therefore sees the resistance of the component plus the resistance of the leads, connections, oxidation, and probe pressure.

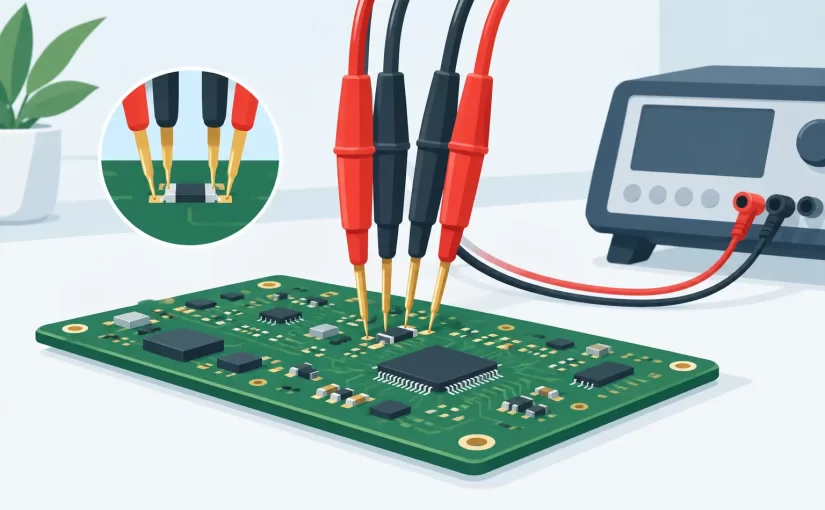
Kelvin probes use two separate pairs of conductors. The force pair applies a known test current to the component. The sense pair measures the voltage directly at the component terminals. Because the sensing input draws very little current, voltage drop in the sense leads is negligible. The instrument calculates resistance from the voltage measured at the device under test and the known test current.

For a two-terminal resistor, the connection order is straightforward: force current enters one terminal and returns from the other, while the sense contacts touch those same two terminals as close to the resistor body or solder joints as possible. Many Kelvin clips and Kelvin test tweezers place force and sense contacts in one compact jaw, making this arrangement faster and more repeatable.

The method does not make every reading automatically accurate. If the sense contacts are placed on a PCB trace several centimeters away from the component, the measured trace resistance is still included. That may be desirable when checking an interconnect, but it is not the same as measuring the component alone.

Select the Right Instrument Mode First

Start by choosing the measurement function that matches the fault or component. A DC low-resistance mode is appropriate for shunts, wiring, contacts, and trace continuity where resistance is the primary concern. An LCR meter is more suitable for inductors, capacitors, and resistors measured at a specified AC test frequency. ESR testing uses an AC method intended to characterize a capacitor’s effective series resistance.

Test frequency matters. A capacitor can show a low ESR at one frequency and a different value at another, particularly with electrolytic, polymer, and ceramic technologies. Inductors and ferrite components can also be frequency-dependent. Use the frequency required by the component specification or the troubleshooting condition, rather than treating a single reading as universal.

Before connecting, check four practical conditions:

  • The circuit is powered down and discharged.
  • The instrument range and test function suit the expected value.
  • The probes, tips, and fixture are clean and mechanically sound.
  • The component can be measured in circuit without a parallel path distorting the result.

A powered circuit can damage an LCR or ESR instrument and produce misleading results. Stored charge in large capacitors is equally problematic. Discharge capacitors through an appropriate resistor and verify the remaining voltage with a suitable meter before applying Kelvin probes.

Compensate the Probes and Fixture

Four-wire measurement reduces lead resistance effects, but compensation is still required for the best results, especially with LCR and ESR measurements. The exact procedure depends on the instrument, but it generally includes open and short compensation.

Open compensation measures residual capacitance and leakage associated with the fixture and probe geometry when the tips are separated. Short compensation measures residual resistance and inductance when the force and sense contacts are connected together at the probe tips. The instrument stores these values and subtracts or corrects for fixture effects during measurement.

Perform compensation using the same probes, tips, and cable arrangement that will be used for the measurement. If you change from Kelvin clips to test tweezers, replace probe tips, or alter a long cable layout, repeat the procedure. At higher test frequencies, even small changes in contact geometry and lead routing can affect parasitic inductance and capacitance.

For low-resistance work, a short check also reveals a damaged lead or contaminated contact. A compensated fixture should produce a stable near-zero reading when its Kelvin contacts are properly shorted. If the value wanders, inspect the probe jaws, cable strain relief, connector seating, and oxidation on the contact surfaces.

Make Contact at the Correct Measurement Plane

The measurement plane is the exact point where the instrument senses voltage. It determines what is included in the result.

When measuring a low-value SMD resistor, place the Kelvin contacts directly on the two solder fillets or on exposed terminal metallization. Avoid contacting distant vias or adjacent copper unless the trace resistance is part of the test objective. For a cable assembly, place the sense contacts at the two points whose resistance must be verified, not at convenient locations farther up the harness.

Contact pressure should be firm enough to break through light surface films but not so high that it damages pads, small components, or conformal coating. On fine-pitch boards, sharp and well-aligned tips are more useful than excessive force. A stable fixture or tweezer-style probe reduces hand movement and helps maintain repeatable contact on 0201, 0402, and similar small packages.

Kelvin probes are especially effective when the force contacts are outside the sense contacts, or when a purpose-built clip maintains the correct geometry. Do not improvise by placing two ordinary probe tips on each terminal unless spacing and stability allow the force and sense points to remain distinct. On small components, dedicated Kelvin tweezers or closely spaced four-wire probe accessories are usually the practical solution.

Measure In Circuit With Caution

In-circuit Kelvin testing is fast, but the board can create parallel paths that are invisible at first glance. A 1 ohm resistor may be connected to other resistors, semiconductor junctions, IC inputs, or copper planes that alter the reading. A capacitor ESR measurement may be influenced by parallel capacitors, regulators, or protection devices.

Use the schematic and board layout to decide whether the reading is meaningful. If the measured value is lower than expected, look for parallel components or alternate current paths. If it is higher, inspect solder joints, cracked terminations, corroded vias, fuses, connectors, and damaged copper. A comparison with an identical channel or known-good board is often more useful than comparing only against a nominal component value.

For critical component verification, isolate one terminal or remove the component. This takes more time but eliminates ambiguity. The appropriate choice depends on the cost of a false diagnosis, the accessibility of the component, and whether the board is a repair unit, production sample, or qualification article.

Reading Low Resistance, ESR, and Inductance Results

A good Kelvin reading is stable, repeatable, and technically plausible. Take several readings while lightly repositioning the probe. If the value changes significantly, suspect contact quality before declaring the component defective. Oxidation, flux residue, worn probe tips, and insufficient jaw alignment commonly cause unstable low-ohm readings.

For resistors, compare the result with the nominal value and tolerance, while accounting for temperature coefficient and in-circuit paths. For current shunts, measure at the intended pad locations because milliohms of copper can matter. For relay contacts or connectors, measure under the specified mechanical state and, where appropriate, under a test current representative of service conditions.

For capacitors, do not interpret ESR without considering capacitance, voltage rating, technology, temperature, and test frequency. A low ESR value is not automatically good if capacitance has fallen substantially. Likewise, ceramic capacitors may have very low ESR while still exhibiting a crack or DC-bias-related performance issue that requires another test method.

Advanced handheld LCR instruments can combine Kelvin-compatible probing with higher test frequencies and component identification functions. In PCB repair, compact tweezer-style measurement can reduce the time required to move from suspected component to verified result, provided the operator still controls the measurement plane and understands the surrounding circuit.

Common Kelvin Probe Errors

The most frequent error is assuming four wires eliminate every source of uncertainty. Kelvin measurement removes most voltage error caused by the force leads, but it cannot correct for poor sense contact, a contaminated pad, thermal effects, electromagnetic interference, or an unsuitable test frequency.

Another common problem is crossing or misidentifying force and sense connections on separate clips. Follow the instrument labeling and keep each terminal’s force and sense contacts paired at the same end of the device under test. On long leads, route force and sense conductors together and avoid large loops that can pick up noise, especially during AC impedance measurements.

Finally, protect the probes. Kelvin tips are precision contacts, not general-purpose scraping tools. Clean them with an electronics-safe method, replace worn points, and verify compensation before measurement sessions where milliohm-level repeatability matters.

A Kelvin probe earns its place on the bench when the difference between a component fault and a connection fault is only a few milliohms. Put the sense contacts at the true test point, compensate the fixture, and let the measurement answer the question you actually need to ask.

Electronics Repair Tools for PCB Diagnosis

A board can look perfect under magnification and still fail because of one 0402 capacitor, a damaged MLCC, or an inductor that has shifted outside its working range. Effective electronics repair tools shorten the path from symptom to component-level evidence. For PCB diagnosis, tool selection is less about owning the largest collection and more about making reliable measurements quickly, safely, and at the frequencies that matter.

Electronics Repair Tools Start With the Measurement Task

A digital multimeter remains the first instrument most technicians reach for. It is appropriate for confirming supply rails, continuity, diode junction behavior, DC resistance, current draw, and basic voltage references. It is not, however, a complete component analyzer. A multimeter may indicate that a capacitor is not shorted while providing no useful indication of its capacitance, ESR, dissipation factor, or behavior at a relevant test frequency.

That distinction matters on densely populated boards. Switching power supplies, RF sections, display drivers, battery-management circuits, and high-speed digital assemblies often depend on small passive components whose faults are not visible through DC checks alone. An LCR meter or ESR meter adds the measurements needed to assess resistors, capacitors, and inductors as components rather than simply as conductive paths.

The correct instrument depends on the failure mode being investigated. If a rail is absent, start with voltage and continuity. If the rail is present but unstable, evaluate the capacitors and inductors supporting that circuit. If a signal path is distorted or intermittent, waveform inspection and analog signature comparison can identify differences between a known-good and suspect section. Good troubleshooting follows the circuit, rather than forcing every question through one meter.

Accuracy Is Only Useful at the Right Frequency

Basic accuracy is a meaningful specification, but it should not be considered in isolation. A 0.1% or 0.2% basic accuracy specification supports confident comparison and verification when the test conditions match the component and application. Test frequency is equally important, particularly for capacitors and inductors.

A capacitor measured at a low frequency can appear acceptable while exhibiting excessive loss or impedance under the operating conditions of a switching circuit. Likewise, inductance readings can vary with frequency, DC bias, core material, and the component’s connection to the surrounding circuit. Instruments with 100 kHz or 250 kHz test capability provide more useful characterization for many modern PCB applications than meters limited to low-frequency measurement.

In-circuit readings still require judgment. Parallel components, semiconductor junctions, control ICs, and alternate current paths can influence the result. A reading that differs from the marking or schematic is not automatically proof of a defective part. Compare equivalent locations where possible, isolate one end of the component when the diagnosis requires certainty, and account for the circuit topology before ordering a replacement.

Direct Access Matters More Than Lead Length

Conventional probe leads are flexible and familiar, but they become inefficient on boards populated with 0201, 0402, and 0603 components. The technician must stabilize the board, place two probes on tiny terminations, avoid bridging adjacent pads, and keep the test contact consistent long enough for the reading to settle. That process is slow, especially during repetitive inspection or production rework.

Tweezer-style LCR instruments address this access problem directly. Insulated tips provide two-point contact at the component terminals, allowing the operator to pick up loose SMD parts or measure accessible devices on the board. The mechanical design is not a convenience feature alone. It improves repeatability by reducing hand movement and making the contact geometry more consistent from measurement to measurement.

For repair work, tip selection also affects results. Fine tips improve access between tightly spaced parts but can be easier to damage. Wider or more durable tips can be better for frequent work on larger passives. Replaceable probing accessories allow one instrument to adapt to bench diagnosis, field service, loose-component verification, and populated-board inspection without compromising the primary measurement method.

Siborg Systems instruments such as Smart Tweezers and LCR-Reader models are designed around this direct-contact workflow, combining handheld SMD access with professional LCR measurement capabilities. The relevant configuration depends on whether the priority is entry-level identification, higher test frequencies, Bluetooth data transfer, or expanded diagnostic functions.

Build a Bench Around Complementary Functions

A capable repair bench does not need duplicate instruments. It needs coverage across the measurements that separate common faults. Start with a quality digital multimeter for electrical safety checks and DC diagnosis, then add specialized tools where they remove uncertainty.

An LCR meter is the primary addition for passive-component work. Look for clear measurement of capacitance, resistance, inductance, ESR, dissipation factor, and impedance, along with selectable test conditions where applicable. Automatic component identification is valuable when sorting unknown loose parts, but manual mode remains important when a specific parameter and frequency are required.

An ESR meter is particularly useful when evaluating capacitors in power circuits. High ESR can cause ripple, poor regulation, startup failure, heat, or intermittent operation even when nominal capacitance appears close to specification. This is especially relevant for electrolytic capacitors, but low-ESR ceramic and polymer capacitors also require measurement conditions appropriate to their application.

Oscilloscope capability belongs on the bench when a fault involves timing, ripple, switching activity, serial communications, or intermittent signal behavior. For compact field work, integrated oscilloscope functions can provide a fast first view. A dedicated bench oscilloscope remains preferable when bandwidth, multiple channels, triggering depth, or detailed waveform analysis is required. The trade-off is straightforward: integrated functions improve portability, while separate instruments provide broader analysis capacity.

Analog Signature Analysis adds another comparison method. By applying an AC stimulus and observing the resulting current-voltage signature, a technician can compare devices or circuit nodes without powering the board. It is not a replacement for LCR measurement or a scope, but it can help locate shorts, opens, leakage paths, and abnormal semiconductor behavior when a known-good comparison point exists.

Protect the Board and the Measurement

Precision instruments cannot compensate for poor probing practice. Before measuring a board, verify the power state, identify energy-storage capacitors, and discharge circuits where necessary. An ESR or LCR measurement performed on a charged capacitor can damage the instrument, the board, or both.

ESD control is equally practical. Use a grounded work surface and wrist strap when handling static-sensitive assemblies, particularly boards containing CMOS logic, RF front ends, memory devices, and fine-pitch controllers. Keep probe tips clean and inspect them for bent points, worn insulation, or contamination that can cause unstable contact.

When troubleshooting powered circuits, choose probes and accessories rated for the voltage and environment involved. Keep one hand clear of the assembly where appropriate, secure the board so it cannot shift, and avoid relying on improvised metal tools near exposed conductors. Fast diagnosis is valuable only when it does not introduce a second fault.

Make Results Repeatable and Defensible

Repair decisions often move beyond the individual technician. Manufacturing teams may need incoming inspection records. Service organizations may need proof of a completed repair. Engineering groups may need to compare a returned board against reference data. In these cases, repeatability and documentation are part of the tool requirement.

Calibration support is one consideration. A NIST Traceable Calibration Certificate provides documented confidence that an instrument has been verified against recognized standards. It does not eliminate the need for careful operation, open and short compensation, or routine inspection of probes and tips. It does provide a traceable basis for measurements used in quality systems, customer reports, and controlled repair processes.

Bluetooth-enabled instruments can further improve workflow when measurements must be captured instead of transcribed. Recording values to a mobile device or PC reduces transcription errors, supports comparison over time, and creates a clearer service record. Wireless transfer is most useful when it fits an established process. For a single loose component, reading the display may be faster. For batch inspection or recurring failure analysis, captured data becomes a practical advantage.

Choose Tools for the Work You Actually Perform

A technician repairing consumer electronics may prioritize portability, SMD access, capacitance, ESR, and diode testing. A manufacturing quality team may place more weight on accuracy, calibration documentation, repeatable fixtures, and data capture. An engineer working with power electronics may require higher-frequency LCR measurement, waveform visibility, and accessories that tolerate larger components and higher-energy environments.

Avoid selecting tools solely by the longest feature list. A high-frequency LCR meter is valuable when the application calls for it, but it may be unnecessary for occasional through-hole repair. Bluetooth is useful when measurements need to be retained, not simply because it is available. The best electronics repair tools are the ones that reduce uncertainty at the exact point where your current workflow slows down.

Keep the bench organized around that principle. Measure the circuit state first, test passive components under meaningful conditions, use direct-contact probes where board density demands them, and document results when the repair must be repeatable. A technician who can trust the measurement can make the next decision with speed rather than guesswork.

Impedance Measurement Guide for PCB Work

A 10 uF ceramic capacitor can appear healthy at 1 kHz and become the source of a power-rail problem at a higher operating frequency. A resistor can measure correctly in DC resistance mode while its parasitic inductance affects a high-speed circuit. This impedance measurement guide focuses on obtaining readings that represent component behavior under real test conditions, not merely a number displayed by an instrument.

What impedance measurement actually measures

Impedance is the opposition a component or network presents to alternating current. It includes resistance and reactance, so it is expressed as a complex quantity with magnitude and phase. Resistance dissipates energy. Capacitance and inductance store and release energy, producing reactance that changes with frequency.

For a resistor, impedance may remain close to its stated resistance over a useful frequency range. For a capacitor, capacitive reactance decreases as frequency rises. For an inductor, inductive reactance increases with frequency. Real components also contain parasitic resistance, inductance, and capacitance, which eventually dominate the result.

That distinction matters during PCB diagnosis. Measuring only DC resistance cannot show capacitor ESR, inductor loss, resonance, or the frequency-dependent loading caused by a component package and its board layout. An LCR meter applies an AC test signal, measures voltage and current, and calculates the selected equivalent parameters at a defined test frequency.

Select the frequency before interpreting the value

A valid impedance reading begins with a relevant frequency. Component data sheets commonly specify capacitance, inductance, dissipation factor, Q, or ESR at a stated frequency and test level. Measuring at a different condition is not necessarily wrong, but it answers a different question.

For general component identification, 100 Hz, 1 kHz, or 10 kHz can be appropriate starting points. Higher frequencies are more useful when evaluating low-value capacitors, small inductors, RF-adjacent circuits, switching power supplies, and the parasitic behavior of SMD components. A 100 kHz or 250 kHz measurement capability can reveal behavior that is hidden at audio-range test frequencies.

The correct choice depends on the fault and the component. A bulk electrolytic capacitor in a low-frequency filter may be assessed effectively at lower frequencies, with ESR included in the evaluation. A multilayer ceramic capacitor supporting a fast digital rail should be checked closer to the frequencies where low impedance is required. Do not expect a single frequency to characterize every component.

Watch for self-resonance

Every physical capacitor and inductor has a self-resonant frequency. A capacitor behaves capacitively below resonance, reaches minimum impedance near resonance, and appears inductive above it. An inductor behaves inductively below resonance and becomes increasingly capacitive above it.

If a reading seems inconsistent with the component marking, check the test frequency before assuming the part has failed. At higher frequencies, a small change in fixture position, lead length, or PCB trace geometry can also affect the measurement.

Choose the right equivalent circuit

Most LCR instruments report component values using series or parallel equivalent circuits. This selection affects the displayed resistance, loss, Q, and dissipation factor, especially when the device under test has significant loss.

A series model represents the component as an ideal reactance in series with a resistance. It is commonly useful for low-impedance capacitors and inductors, where lead resistance, winding resistance, or ESR is naturally modeled in series. A parallel model represents an ideal reactance alongside a resistance and is often appropriate for high-impedance components and leakage-dominated behavior.

As a practical rule, use the model specified by the component manufacturer whenever possible. If no specification is available, compare the measured impedance magnitude with the instrument’s applicable model guidance. Recording only “10 nF” is incomplete when loss and frequency are relevant. Record capacitance or inductance, the selected series or parallel mode, test frequency, and the associated ESR, D, or Q value.

Establish a controlled measurement setup

The instrument, fixture, and operator form part of the measurement system. This is particularly true for milliohm-level ESR, low-inductance capacitors, and small SMD parts. Poor contact pressure or oxidation can produce an apparent component defect.

Start by allowing the meter to stabilize according to its operating instructions. Use the shortest practical test path and select probes or tweezers that match the component size. Dedicated tweezer-style contacts reduce loop area and make it possible to contact opposing SMD terminations directly, rather than chasing a small part with conventional test leads.

Perform open and short compensation with the same fixture and approximate measurement geometry used for the test. Open compensation reduces the influence of stray capacitance. Short compensation reduces residual lead resistance and inductance. Compensation is not optional housekeeping when measuring very small values. It is the reference that separates the fixture from the device under test.

For repeatable production or laboratory work, control contact location and pressure. A probe touching the end cap of a chip capacitor may not produce the same result as one contacting a nearby solder fillet, especially at higher frequencies. Use a holder, fixture, or consistent technique when measurements will be compared across operators or lots.

Measure loose parts first when possible

A loose component measurement provides the clearest indication of the part itself. Remove the component from static-sensitive packaging only with suitable ESD controls, identify its value and package, compensate the fixture, and take readings at the frequencies that match the intended application or data sheet conditions.

For loose parts, confirm more than the nominal value. A capacitor may show the correct capacitance but excessive ESR. An inductor may measure its stated inductance but have poor Q or higher-than-expected winding resistance. A resistor can pass a low-frequency resistance check while showing unexpected inductive behavior at the circuit’s operating range.

Smart Tweezers and LCR-Reader instruments are designed for this direct-contact workflow, allowing technicians to identify and measure SMD components without changing from long test leads to a separate fixture. The benefit is not just speed. Short, controlled contacts reduce the uncertainty added by loose probe wiring.

Understand the limits of in-circuit impedance tests

In-circuit testing is fast, but the reading represents every available path connected to the probes. A capacitor measured across a power rail may be in parallel with several other capacitors, integrated circuits, protection devices, and converter stages. A resistor can be shunted by another branch. An inductor can be affected by semiconductor junctions or transformer windings.

Use in-circuit impedance measurement as a diagnostic comparison tool. Compare identical channels, known-good boards, or equivalent locations on the same board. A significantly lower impedance on one rail may indicate a shorted capacitor or semiconductor. A substantially different ESR reading may identify a degraded capacitor, but confirm the result after isolating the part if parallel paths are plausible.

Power must be removed before ordinary passive-component measurement. Discharge capacitors safely and verify that stored voltage is absent. An energized board can damage the instrument, create misleading readings, or place an active circuit in an unintended state.

A practical isolation strategy is to lift one terminal only when necessary. This removes most parallel ambiguity while minimizing rework compared with complete removal. For dense assemblies, inspect the schematic or board topology first. Knowing which components share a node prevents wasted troubleshooting time.

Read ESR, D, and Q in context

ESR is especially useful for capacitors in power conversion, filtering, and decoupling roles. High ESR increases ripple voltage, heat, and losses. However, a low ESR value is not automatically good if it is inconsistent with the capacitor technology or if the measurement frequency is inappropriate.

Dissipation factor, or D, expresses loss relative to reactance. Lower D generally indicates lower loss in capacitive measurements. Quality factor, Q, is the inverse relationship used frequently for inductors and resonant components. A falling Q can point to core loss, winding loss, damage, or test conditions outside the part’s intended range.

Use the specification as the acceptance limit whenever one exists. Generic pass-fail values are unreliable because a polymer capacitor, aluminum electrolytic, MLCC, ferrite inductor, and air-core coil are designed for different impedance and loss characteristics.

Document measurements that others can use

A useful record includes the component reference designator, nominal value, measured value, test frequency, test level if available, equivalent circuit mode, fixture compensation status, and whether the test was in circuit or out of circuit. Add board revision and ambient conditions for failure analysis or quality work.

Bluetooth or PC-connected measurement tools can reduce transcription errors when many readings must be captured, compared, or attached to a service report. Digital capture is most valuable when it preserves the conditions behind the number. A spreadsheet of capacitance values without frequency, mode, and test location can be difficult to interpret later.

Accurate impedance work is a matter of matching the meter, frequency, fixture, and circuit context to the question being asked. When a result is surprising, treat it as evidence to investigate rather than an immediate verdict on the component.

LED Testers for Accurate PCB Diagnostics

A dim display, an intermittent status indicator, or a dark LED backlight strip can turn a straightforward repair into an extended fault-isolation job. LED testers reduce that uncertainty by applying a controlled test stimulus directly to the device or LED string, revealing polarity, illumination, and approximate forward voltage without requiring a powered circuit.

For PCB repair, production inspection, and field service, the useful question is not simply whether an LED lights. The instrument must apply an appropriate voltage and current, provide a meaningful reading, and let the operator reach the component without damaging fine pads, neighboring parts, or the LED itself.

What LED Testers Actually Measure

At the component level, an LED is a diode with a light-emitting junction. A tester forward-biases that junction. When the applied voltage exceeds the LED’s forward-voltage requirement and current is limited to a safe value, the device emits light. Reversing the connection should normally produce no illumination.

A basic LED test therefore establishes three practical facts: whether the device conducts in the expected direction, whether it emits light, and the approximate forward voltage at the applied current. These results are often enough to identify an open LED, reversed installation, damaged bond wire, or incorrect replacement part.

Forward voltage is not a fixed identification number. It varies with LED chemistry, current, junction temperature, binning, and optical color. A red indicator LED may conduct at a substantially lower voltage than a white or blue LED, while infrared emitters can function normally without visible light. Treat the displayed voltage as a diagnostic measurement, not as a complete part specification.

A multimeter diode mode can test many discrete LEDs, but it may not supply enough voltage to illuminate white, blue, ultraviolet, or series-connected LEDs. Dedicated instruments may provide a higher test-voltage range for these applications. That capability is valuable, but it also demands controlled current and disciplined probing.

Why Test Current and Voltage Range Matter

LEDs are current-driven devices. Once forward-biased, a small voltage change can create a significant change in current. A useful tester limits current rather than leaving the operator to infer safe conditions from an open-circuit voltage rating.

Low-current test modes are generally preferred for small indicator LEDs, SMD LEDs, and LEDs tested in sensitive assemblies. They can confirm conduction and polarity while reducing stress on the junction. A higher-voltage mode is necessary when checking multiple LEDs in series, such as display backlight strips, but the tester should still regulate current to prevent excessive dissipation.

Higher range is not automatically better. Applying a high-voltage LED test to a single small SMD LED can create unnecessary stress if the instrument’s current limit is unsuitable. Conversely, a low-range diode test can falsely suggest that a healthy white LED or a multi-LED string is open because the meter cannot reach its required forward voltage.

The correct mode depends on the device under test. Use low current and direct probes for individual board-mounted LEDs. Use a controlled higher-voltage range for strings only after confirming the string topology and disconnecting or isolating circuitry when required.

Reading a Dim or Uneven Result

An LED that lights dimly is not necessarily defective. Test current may be deliberately low, and some packages distribute light in a way that is difficult to see from a particular angle. Compare like components using the same test mode and viewing conditions.

Uneven brightness across a string can be more informative. A noticeably dim device, a device that requires a different voltage, or one that flickers during gentle probe movement may point to junction degradation, cracked solder joints, contamination, or a damaged trace. Repeat the test to separate a repeatable electrical result from an unstable mechanical connection.

In-Circuit LED Testing Has Limits

Testing an LED on a populated PCB is fast, but the surrounding circuit can change the result. Parallel diodes, driver IC outputs, protection networks, capacitors, and alternate current paths may make a good LED appear shorted, open, or unusually low in forward voltage.

Start with the board unpowered unless the service procedure specifically calls for powered measurements. Disconnect batteries, external adapters, and stored-energy sources. A tester’s applied voltage can interact unpredictably with active circuitry, particularly in LED drivers and display modules.

If an in-circuit measurement is ambiguous, compare it with an identical channel or neighboring LED. Symmetry is often the most useful reference in a repeated circuit. If no comparison point exists, isolate one LED lead or remove the component for a definitive test. That extra step is slower, but it avoids replacing a functioning part because of a misleading in-circuit path.

Backlight assemblies deserve special caution. Some strips contain integrated protection elements, multiple dies, or series and parallel arrangements that do not behave like a single discrete LED. A string tester can quickly identify whether a strip conducts and illuminates, yet it may not identify every marginal LED in a complex assembly. Localized voltage comparison and visual inspection remain useful follow-up methods.

Probe Access Determines Diagnostic Speed

The electrical capability of LED testers matters only when the probes can contact the device reliably. Conventional pointed leads are practical for through-hole LEDs, exposed test pads, connector pins, and larger strips. Fine SMD LEDs often require more controlled contact.

Sharp probes can slip off small pads and bridge adjacent conductors. For fine-pitch PCB work, insulated needle probes, spring probes, or tweezer-style accessories give better positional control. The goal is firm contact with minimal force. Pressing hard enough to flex a board can temporarily restore a cracked joint and conceal the fault being investigated.

Probe placement also affects the reading. Contact the actual LED terminals or known points in the same electrical path. Testing across a resistor, driver transistor, or connector section may show a voltage response without proving that the LED junction is intact. Board layouts, polarity marks, and circuit documentation should guide the measurement whenever available.

For production or recurring repair work, a repeatable fixture can be more valuable than faster handheld probing. A fixture establishes consistent contact pressure, orientation, and test conditions, improving pass-fail decisions across batches. Handheld tools remain the better choice for rework, field diagnostics, and varied board geometries.

Selecting LED Testers for the Workbench

Choose an instrument based on the LED types and failure modes encountered most often. A technician repairing consumer displays needs controlled higher-voltage testing for strips and modules. A PCB rework specialist may place greater value on low-current component testing, fine probes, and a compact form factor. Manufacturing teams may prioritize repeatable test conditions and documented inspection procedures.

Evaluate the instrument’s maximum test voltage, current-limit behavior, polarity indication, display readability, and supported LED configurations. Confirm whether the tester is intended for individual LEDs, series strings, or both. A visible-light result alone is insufficient when servicing infrared, ultraviolet, or enclosed optical devices, where current and voltage readings carry more diagnostic weight.

It is also useful to separate LED verification from broader component analysis. A dedicated LED function establishes junction behavior quickly. An LCR meter, ESR meter, or digital multimeter addresses the resistors, capacitors, inductors, supply rails, and driver components that may be responsible when a known-good LED does not operate in the circuit.

Siborg’s component-testing approach is built around direct access to small devices on boards, where probe control and repeatable measurements can save more time than a general-purpose test setup. For LED diagnostics, that same discipline applies: test the junction first, then follow the circuit path when the result does not match the observed failure.

A Practical Test Sequence

Begin by inspecting the LED and surrounding area under magnification. Look for discoloration, cracked lenses, lifted pads, corrosion, missing components, and thermal damage. Then verify the board is unpowered and select the lowest appropriate test mode.

Connect the probes with attention to polarity and observe both illumination and the electrical reading. Reverse the probes to confirm expected blocking behavior. If the LED is in circuit, compare it to a matching device or channel before declaring it defective.

When testing a series string, begin with the controlled string-capable mode and watch for partial illumination, flicker, or an unexpected voltage requirement. If the result is unclear, divide the string into smaller sections rather than increasing test stress. This approach narrows the fault while protecting uncertain components.

A reliable LED test is a measured decision, not a brightness check. Use controlled current, select a voltage range that matches the assembly, and treat every in-circuit result in the context of the surrounding design. That discipline turns a small handheld tester into a practical tool for finding faults before they become unnecessary board replacements.

Precision Multimeters for PCB Troubleshooting

A 3.3 V rail reading of 3.28 V may be completely acceptable. A 1.000 V reference reading of 0.982 V may identify a failed regulator, a loaded reference node, or a measurement setup problem. The difference is not simply the number of display digits. Precision multimeters help technicians determine whether a measured value is meaningful enough to support a repair, production, or design decision.

For populated PCB work, a meter must do more than measure voltage. It must maintain a known level of accuracy, avoid disturbing sensitive circuits, respond predictably to changing signals, and provide repeatable readings when probes move between small test points. Selecting the right instrument starts with understanding what precision means in the measurement path.

What Makes a Multimeter Precise?

A precision multimeter is defined by more than high resolution. Resolution is the smallest change the display can show. Accuracy describes how close the indicated value is expected to be to the actual value, within stated conditions. A meter may display 10.000 V while its accuracy specification permits a much wider error band than the final digits suggest.

Basic DC voltage accuracy is usually the first specification to examine because voltage is the reference measurement for most electronic troubleshooting. A 0.1% basic accuracy specification provides a substantially tighter starting point than a general-purpose meter specified at 0.5% or 1%, particularly when checking low-voltage power rails, sensor outputs, reference circuits, or analog control nodes.

The complete accuracy statement matters. It commonly includes a percentage of reading plus a number of counts. On a 1.0000 V measurement, an accuracy of ±(0.1% of reading + 2 counts) is not identical to a flat ±0.1%. Range selection, display resolution, temperature, battery condition, calibration interval, and signal frequency can all affect the usable result.

Input impedance is equally relevant. A high-impedance voltage input draws very little current and reduces loading on the circuit under test. That is useful at high-resistance divider nodes, CMOS logic inputs, reference outputs, and low-current sensor circuits. It does not mean every reading is automatically valid. A floating node can display a plausible voltage through leakage, capacitive coupling, or internal protection paths. In those cases, a technician may need to apply a controlled load, compare readings at adjacent nodes, or inspect the signal with an oscilloscope.

Precision Multimeters and the PCB Workflow

On a bench, measurement quality depends on the instrument, probes, access method, and the circuit state. Standard 4 mm probes are effective for connectors, test pads, and power terminals. They are less efficient when probing 0402 and 0201 components, fine-pitch IC pins, or dense assemblies where a probe slip can short adjacent conductors.

For board-level repair, the fastest workflow often combines tools rather than forcing one meter to perform every task. A precision multimeter verifies DC rails, continuity, diode drops, resistance, current, and often frequency or capacitance. A dedicated LCR meter or SMD test tweezers identify resistors, capacitors, and inductors directly at the component. An oscilloscope establishes whether a voltage is stable, switching, noisy, or pulsed.

This distinction prevents a common diagnostic error: treating an in-circuit component reading as an isolated component value. Parallel paths can lower a resistance measurement. Semiconductor junctions can alter the apparent value. Capacitors can charge from the meter’s test stimulus. A stable, repeatable result is useful evidence, but it must be interpreted against the schematic and the surrounding circuit.

Siborg’s component-focused instruments are designed for this complementary role. Tweezer-style contact can shorten the time required to identify small passive parts on populated boards, while a precision DMM remains the appropriate tool for checking the operating voltages and circuit conditions around them.

Accuracy Must Match the Decision

Not every measurement warrants a high-accuracy instrument. If a 24 V relay supply is either present or absent, a conventional meter may be sufficient. If a 2.500 V precision reference feeds an ADC, an error of a few millivolts can be consequential. The correct question is not whether the meter is labeled precision, but whether its total uncertainty is comfortably smaller than the tolerance being evaluated.

Consider a 1.8 V processor rail with a ±3% tolerance. The acceptable range is 1.746 V to 1.854 V. A meter with modest accuracy may confirm that the rail is broadly correct. Now consider a calibration fixture verifying a 1.800 V source to within ±2 mV. Resolution, basic accuracy, temperature coefficient, calibration status, and probe connection quality become central to the measurement.

A practical rule is to aim for instrument uncertainty substantially below the allowed circuit tolerance. The required margin depends on the risk of a false pass or false fail. Production and quality-control environments usually require more margin and clearer documentation than initial bench troubleshooting.

Specifications That Deserve Attention

The specification sheet should be read as an operating document, not a feature list. For precision multimeters, four areas deserve close attention:

  • DC voltage accuracy and resolution: These establish the confidence available for power rails, references, battery systems, and sensor outputs. Check the exact range used, not only the headline accuracy figure.
  • AC bandwidth and true-RMS behavior: A reading taken on PWM, switching supplies, variable-frequency drives, or distorted waveforms can be misleading when the meter’s bandwidth or crest-factor limits are exceeded. True RMS is useful only within its stated frequency and amplitude limits.
  • Resistance and continuity test current: Low-ohms work is sensitive to lead resistance and contact pressure. Higher resistance ranges can be influenced by contamination, moisture, flux residue, and circuit leakage. Continuity response time also affects whether intermittent faults can be located efficiently.
  • Safety ratings and input protection: CAT ratings must correspond to the measurement environment. A meter suitable for low-energy PCB work is not automatically appropriate for distribution panels, industrial mains, or high-fault-current locations.

Current measurement deserves special caution. Measuring current requires opening the circuit and placing the meter in series. The burden voltage introduced by the meter can reduce the voltage available to the load and alter the behavior being investigated. For low-current battery products, this can create a false impression of normal or abnormal consumption. A current probe, shunt resistor measured with a differential method, or a dedicated low-burden measurement mode may be a better choice when the circuit is sensitive.

Calibration, Repeatability, and Real Bench Conditions

A precision measurement is only as useful as its traceability. Calibration establishes the relationship between the meter’s reading and recognized standards at the time of test. A NIST Traceable Calibration Certificate provides documented traceability for organizations that need to support quality systems, service records, or controlled test procedures.

Calibration does not eliminate day-to-day technique errors. Worn probe tips, oxidized contacts, weak batteries, thermal drift, and poor lead placement can dominate the uncertainty of a small measurement. Before investigating a suspected low-resistance fault, short the leads and observe the residual value. Use the relative function if appropriate, or account for the lead resistance manually. For voltage work, inspect the probe tips and verify the meter against a known source when the result will drive a costly decision.

Temperature also matters. A meter brought in from a cold vehicle, or used beside a rework station, may not be at the ambient condition assumed by its accuracy specification. Let the instrument stabilize when checking tight tolerances. In production, consistent fixture contact and a defined warm-up period improve repeatability more than adding display digits.

When a Multimeter Is Not the Right Tool

Precision multimeters are highly capable, but they do not replace waveform analysis or impedance measurement. A DC reading cannot reveal ripple that is causing a microcontroller reset. An AC reading may not characterize a narrow switching transient. Resistance mode cannot reliably identify a capacitor’s ESR, an inductor’s test-frequency behavior, or the value of a part heavily influenced by parallel circuitry.

Use an oscilloscope when timing, ripple, transients, duty cycle, or startup behavior matters. Use an LCR meter when capacitance, inductance, dissipation factor, or test frequency is part of the question. Use component test tweezers when direct access to small SMD parts is the limiting factor. The most efficient bench is not the one with a single instrument for every job. It is the one where each instrument answers its measurement question with defensible uncertainty.

Before accepting a critical reading, pause at the probe tips: confirm the range, the reference point, the expected tolerance, and whether the circuit itself can be affected by the test. That short check turns a precise number into useful engineering evidence.